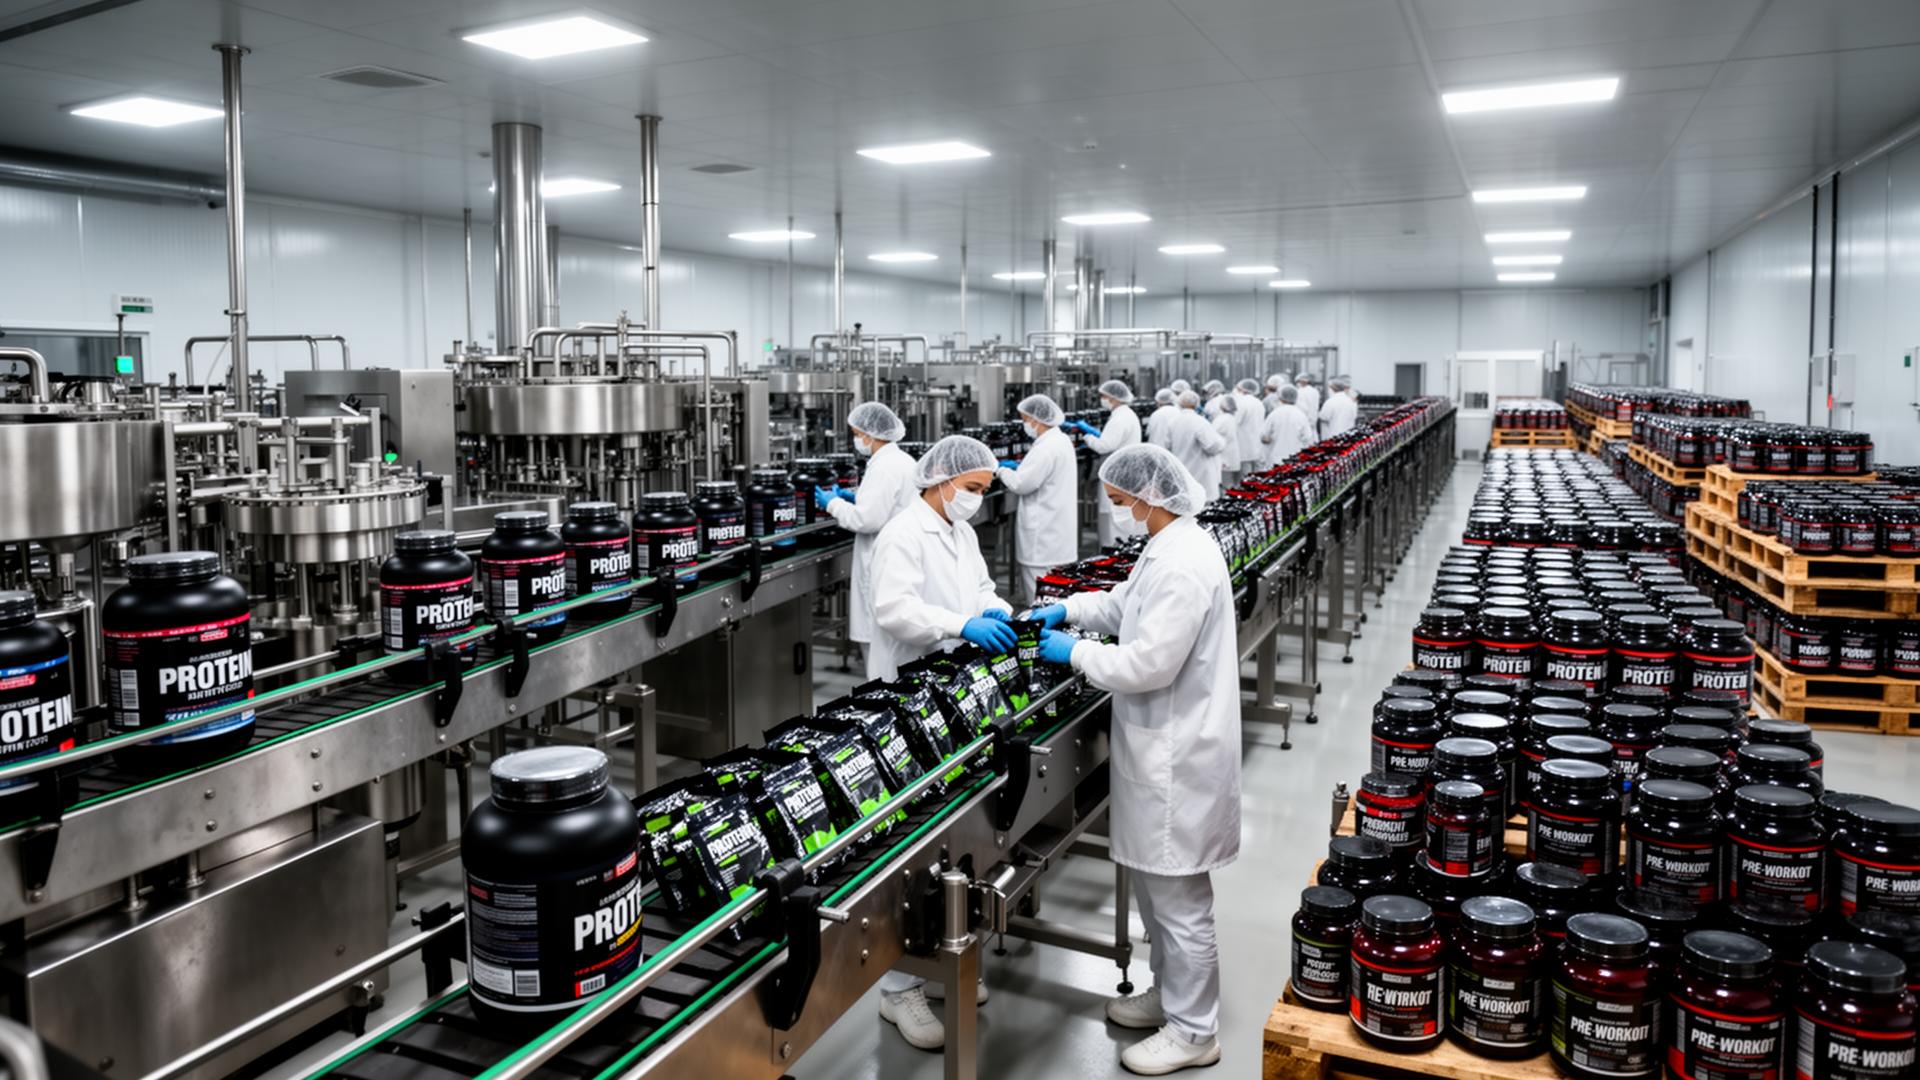
Why Significant Scale Is the Ultimate Edge for Private Label Sports Nutrition Manufacturing
In an industry where every cent and every day counts, size isn't just impressive — it's your competitive superpower. A lot of manufacturers talk about quality. The ones actually delivering consistent wins for ambitious sports nutrition brands operate at a scale that unlocks lower costs, faster turnaround, and a level of reliability smaller players simply can't match.
Picture the version of your brand that lives 12 months out.
Your new pre-workout or protein line hits shelves the exact week the trend peaks. Pricing stays aggressive because your manufacturing partner isn't passing along the overhead of tiny batches. Every pouch, bottle, and sachet arrives with the kind of premium feel athletes notice — because the partner behind it invested years ago in world-class equipment, rigorous in-house testing, and deep category expertise across creatine, whey, plant proteins, and full-stack formulas.
That's not luck. That's scale doing the heavy lifting.
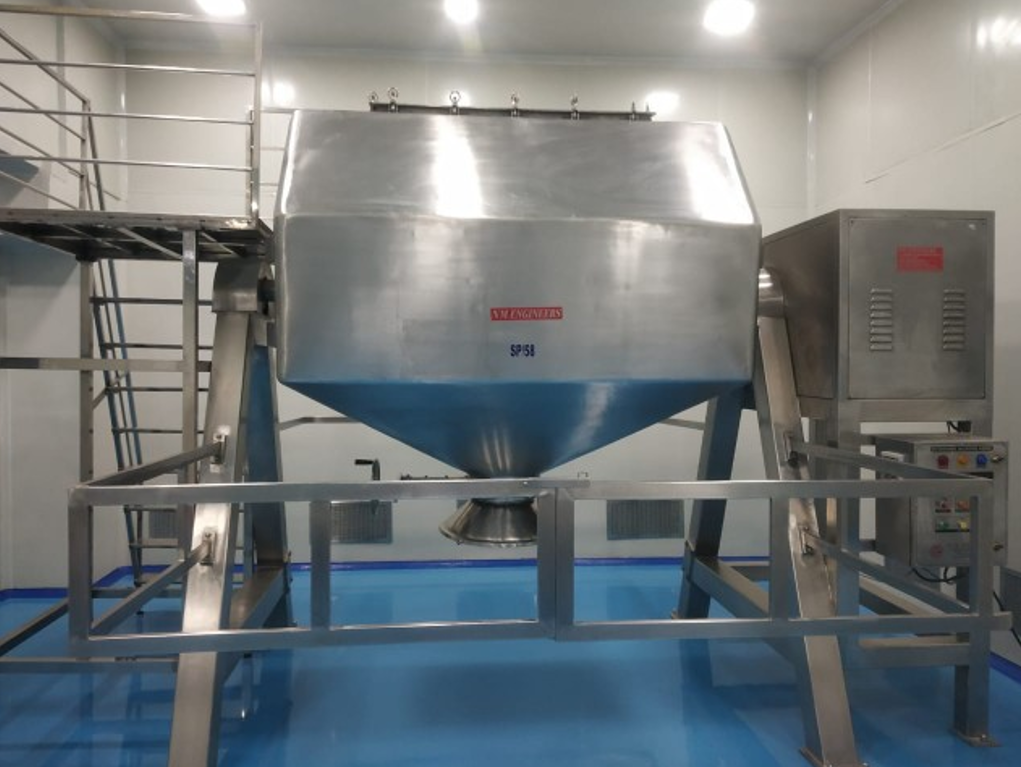
The Advantages Smaller Players Genuinely Can't Match
Superior pricing power. High-volume raw material purchasing and optimized production lines slash costs on creatine, whey isolates, BCAAs, beta-alanine, electrolytes, and full-stack formulas — and those savings flow straight into your margin instead of disappearing into a small co-packer's overhead.
Unrivaled speed and flexibility. From custom formulations to ready-to-launch stock options — pre-workouts, recovery blends, creatine gummies and powders, plant-based proteins — large facilities move from concept to first pallet faster, without sacrificing GMP standards along the way.
Consistent quality at any volume. Advanced automation, in-house testing labs, and multi-line redundancy mean your product performs the same whether you order 500 units or 500,000. The customer can't tell which batch they got — and that's the entire point.
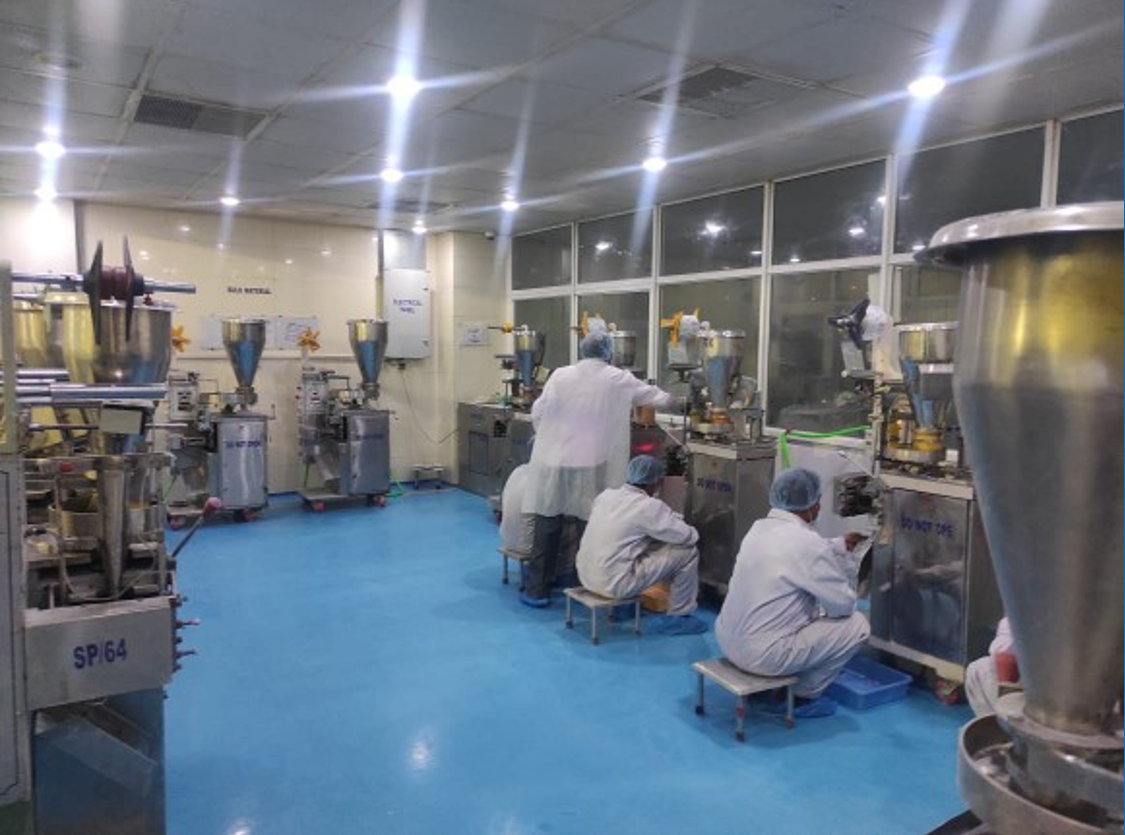
End-to-end support. Formulation, flavor masking, stability testing, innovative packaging (sachets, tubs, stick packs, barrier bottles), labeling compliance, and logistics — all under one roof. No finger-pointing between five vendors when something goes sideways.
Risk reduction and growth readiness. Scale absorbs sudden demand spikes — the viral TikTok pre-workout moment, the unexpected retailer expansion, the seasonal pull — while keeping per-unit economics favorable as you push into new countries.
What This Means for the Brand You're Building
Sports nutrition moves fast. Athletes demand proven, great-tasting products at accessible prices — and they have zero patience for a brand that runs out of stock, ships inconsistent flavors, or quietly raises prices because their manufacturer just did.
Brands that partner with a large-scale private label expert stay agile, profitable, and free to focus on what they actually do best: building loyalty, telling their story, and growing a community. The manufacturing piece just… works.
Don't let limited manufacturing capacity hold your brand back. Partner with scale — and turn ambitious ideas into market-leading reality.
Tell us what you're building below. Our private label manufacturing partner will be in touch with pricing, MOQs, and timelines that respect both.